
Flute and chip space
Choose flute count and helix with the slot width, radial engagement and chip evacuation method in mind.
APPLICATION · ALUMINUM
Aluminum milling rewards clear chip evacuation and a tool geometry matched to the alloy, temper and material-removal target. Record the feature and machine limits before choosing a cutter.
DIRECT ANSWER
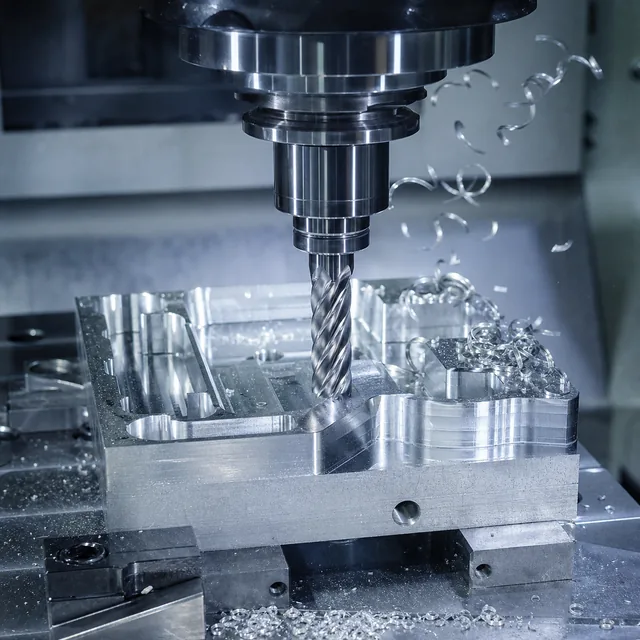
For aluminum milling, choose the BOFA tool from the alloy and temper, chip-space requirement, engagement and spindle limit. Separate roughing from finishing, state the coolant or air method and validate burrs and chip evacuation on the actual machine.
QUERY FAN-OUT COVERAGE
| Field | What to record |
|---|---|
| Sample size | No public BOFA sample count is claimed; record the number of pockets, slots or test parts used for comparison. |
| Test environment | Use the actual spindle limit, holder, workholding, coolant or air blast and chip evacuation arrangement. |
| Controlled variables | Keep alloy and temper, tool geometry, diameter, flute count, engagement, stick-out and toolpath revision explicit. |
| Measurements | Record burr height or condition, built-up material, surface result, spindle load and chip evacuation. |
APPLICATION BRIEF
These are selection inputs, not blanket cutting claims. Confirm the exact series chart and the actual machine setup before production.
Cast and wrought aluminum alloys. Include the alloy family, temper and silicon or abrasive condition when known.
High-removal pocketing, slotting, adaptive roughing, shoulder milling and finishing. State whether chip evacuation or surface finish is the primary constraint.
SELECTION CHECKS
Put the following decisions in the same document as the drawing or sample. It keeps engineering, purchasing and quality aligned.
Choose flute count and helix with the slot width, radial engagement and chip evacuation method in mind.
Keep the gauge length short; specify wall height and the longest unsupported reach required.
State flood, mist, through-tool coolant or air blast so chip evacuation assumptions are explicit.
Separate roughing allowance from the finishing pass and state the required surface or burr condition.
PUBLISHED PRODUCTS
PEOPLE ALSO ASK
Answers describe the information needed for a sound decision. They do not replace the tool maker’s chart or a controlled first pass.
Flute count depends on the alloy, slot width, radial engagement, spindle speed and chip evacuation. Use the exact series chart and state whether the cut is a full slot or side milling.
Check edge sharpness, runout, toolpath direction, workholding and the finishing allowance. A stable setup and a geometry intended for the alloy are more reliable than one universal parameter.
Send alloy and temper, tool diameter and reach, flute preference, engagement, machine and holder interface, coolant or air method, finish target, quantity and drawing.
READY TO COMPARE?
Attach the drawing, current tool photo or process notes. BOFA will confirm the series, interface and quotation route.
Open technical RFQ →TECHNICAL SELECTION NOTES
Use these notes to frame a first selection. Final cutting data must come from the exact BOFA series chart and a controlled test on the target machine.
Aluminum selection is controlled by alloy, temper, chip evacuation and the material-removal target. The right flute arrangement is the one that keeps the chip moving without sacrificing the required finish.
Published cutting data only becomes useful when the machine and engagement assumptions are known.